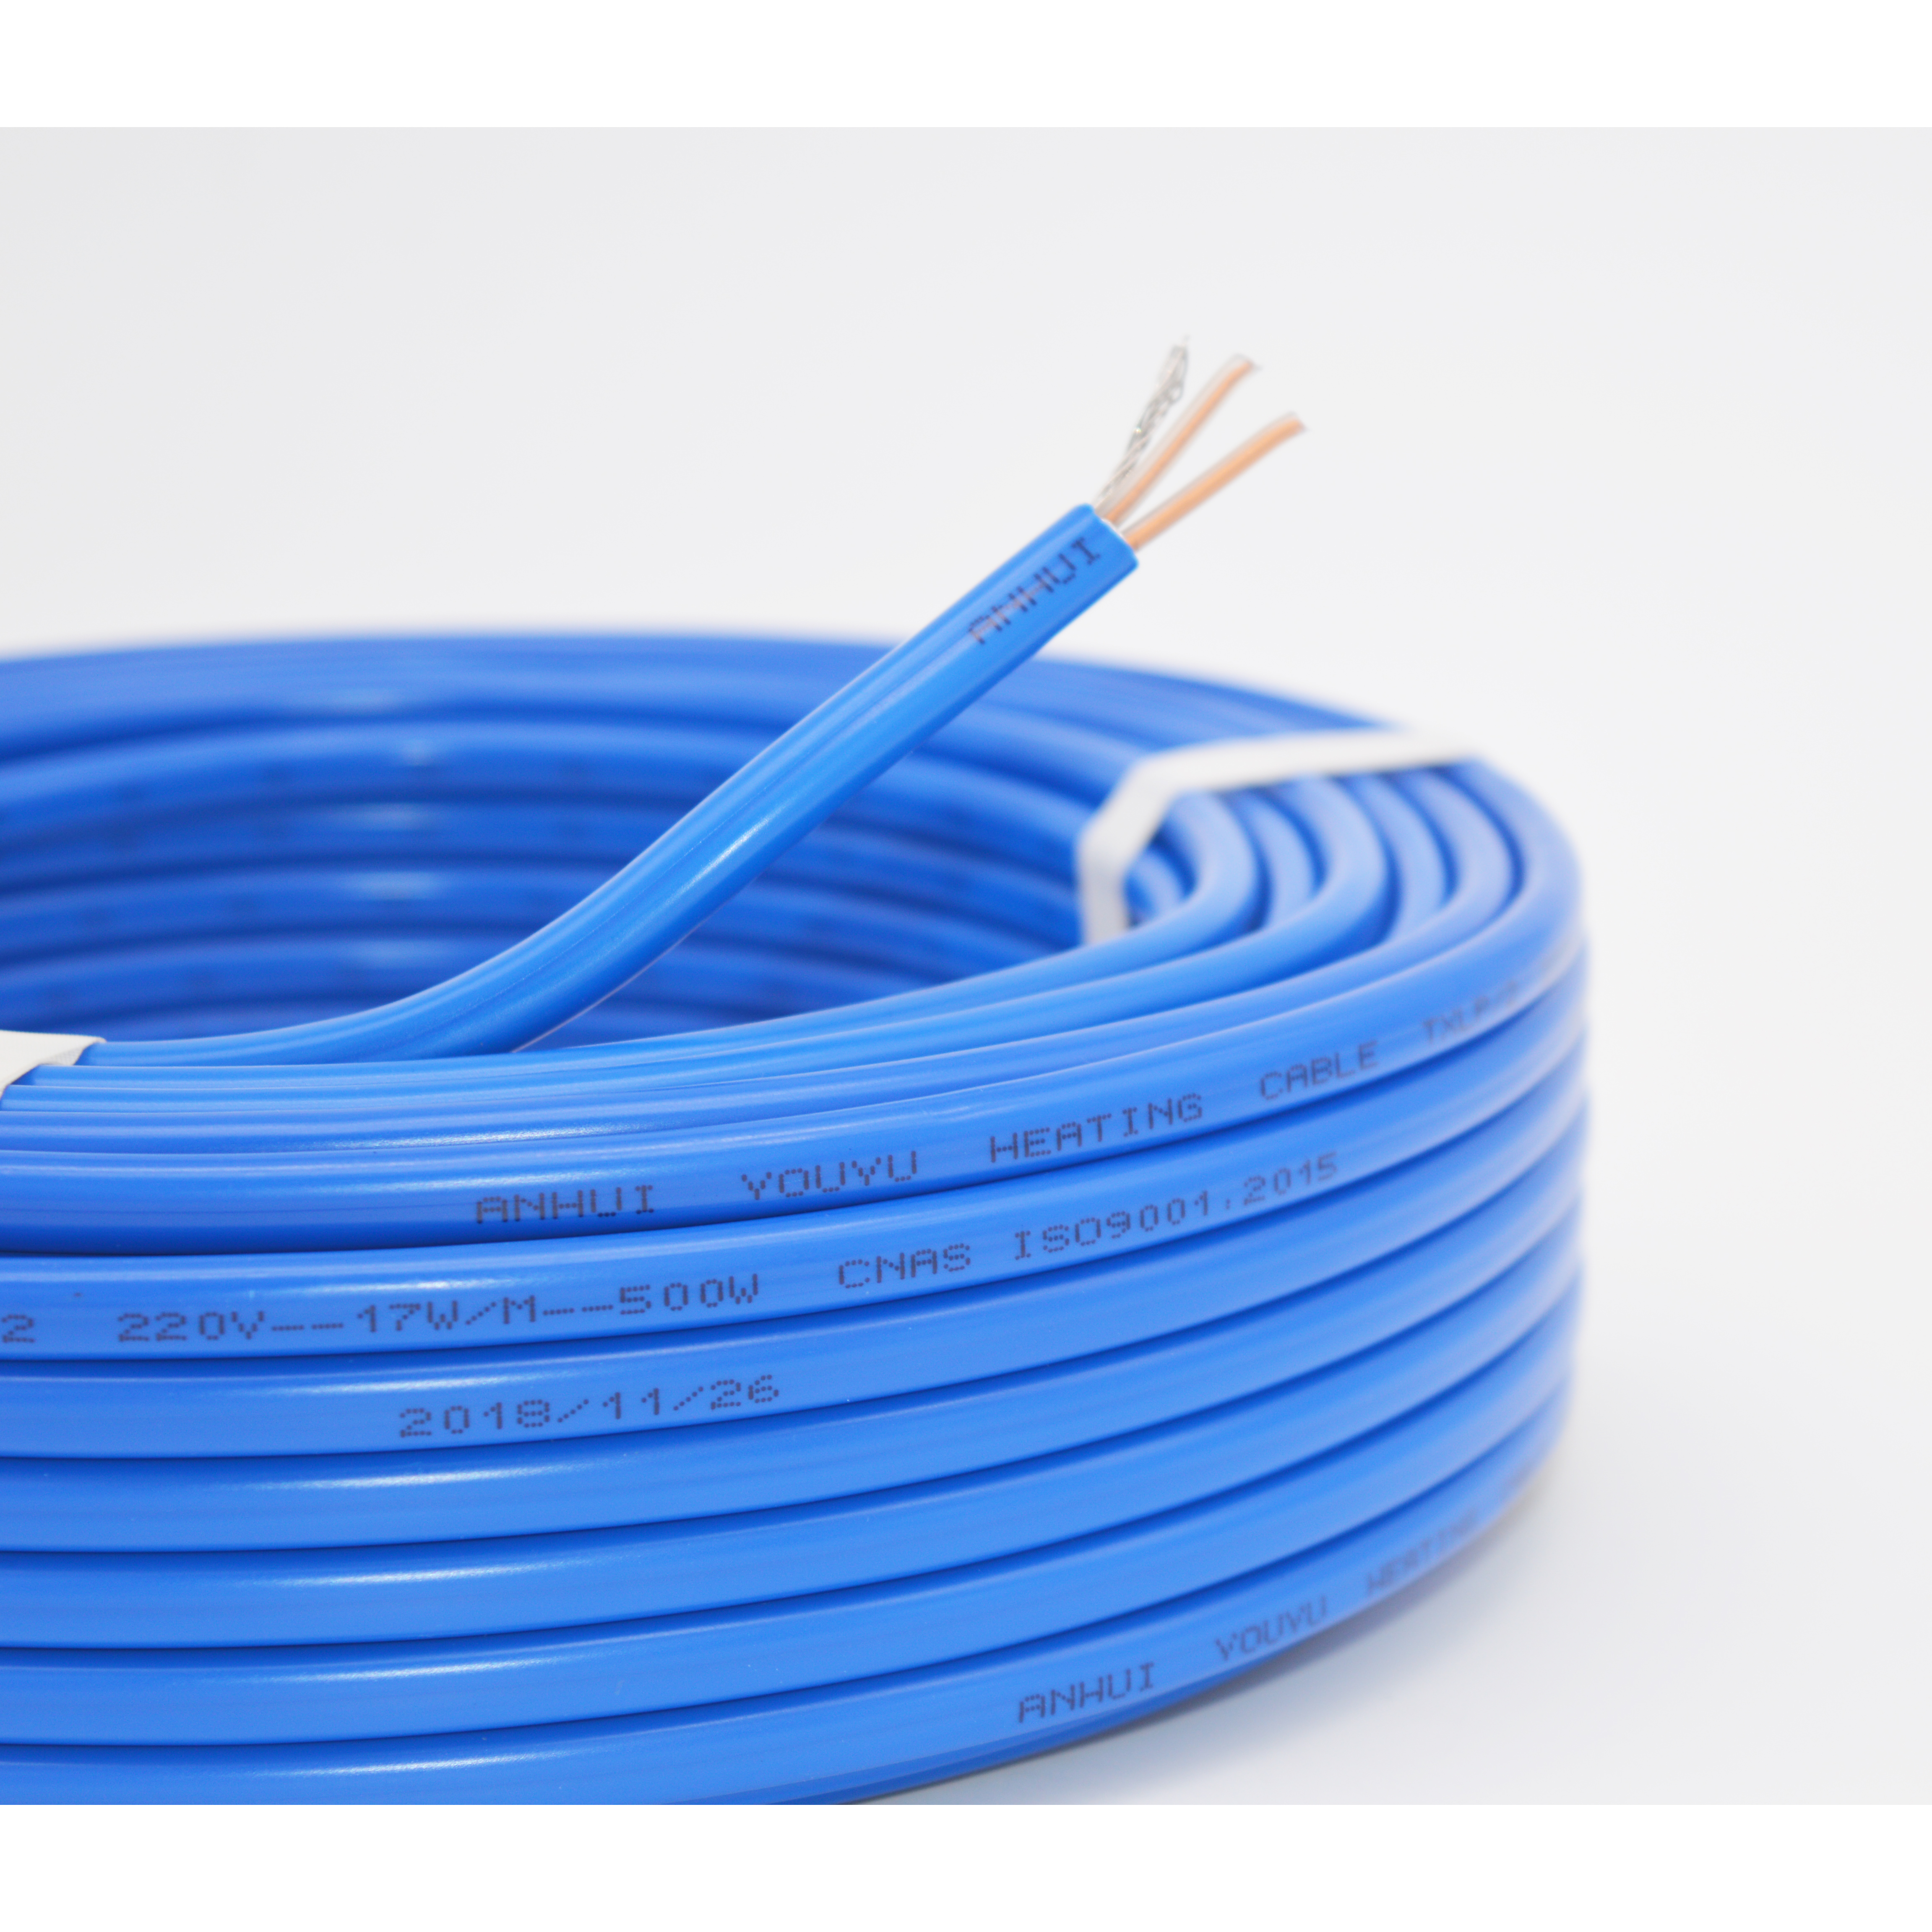
Industrial pipeline operation faces severe challenges in low-temperature winter environments. Liquid media such as water, crude oil, and chemical solutions are prone to condensation, freezing, and blockage in cold weather, leading to pipeline rupture, production shutdown, and huge economic losses. For industrial enterprises and facility managers, choosing a stable and durable heating solution is the key to ensuring year-round normal operation, and heat trace cable has become the most mainstream and reliable anti-freezing and heat-preserving product in the industrial field.
Many industrial buyers confuse ordinary heating tapes with professional heat trace cable. Civilian heating products are only suitable for simple household pipeline anti-freezing and cannot adapt to high-pressure, corrosive, and low-temperature industrial working conditions. Industrial-grade
heat trace cable features high-strength outer sheath, anti-corrosion, anti-aging, and explosion-proof properties, which can operate stably in harsh environments such as chemical plants, steel mills, and energy stations for a long time.
Different from single-functional heating products, qualified industrial heat tracing systems need to match precise power design and safety certification. Regular products on the market often lack ATEX explosion-proof, EAC, and ISO system certifications, which will bring great safety hazards to industrial production. Trace heating cable manufactured by professional manufacturers strictly complies with international safety standards, covering self-regulating, constant wattage, and MI mineral-insulated models, fully meeting the differentiated needs of various industrial scenarios.
Self-regulating trace heating cable is the most widely used type in industrial light-load scenarios. It can automatically adjust heat output according to ambient temperature, avoiding energy waste caused by continuous high-power operation. When the external temperature drops sharply, the cable increases heat output to ensure that the pipeline medium does not freeze; when the temperature rises, it intelligently reduces power consumption, achieving the dual goals of anti-freezing and energy saving. In addition, it supports safe overlapping installation, which is very suitable for complex pipeline layouts with elbows, valves, and joints.
In heavy industrial scenarios such as petrochemical and natural gas transmission, MI mineral-insulated heat trace cable is more popular. It has ultra-high temperature resistance and explosion-proof performance, can withstand extreme low temperatures and high-pressure working environments, and has a service life of up to 25 years, far exceeding ordinary heating cables. This type of product is widely used in key projects such as pipeline heat tracing in iron and steel plants and data room temperature control.
Many customers consult the difference between industrial heat trace cable and civilian
pipe heating cable. In short, pipe heating cable is mainly used for residential water pipes, sewer pipes, and agricultural irrigation pipelines, focusing on basic anti-freezing functions; while industrial trace heating cable focuses on precise temperature maintenance and safe operation of industrial media, with higher requirements for safety, durability, and environmental adaptability.
For enterprises that need both industrial pipeline protection and indoor renovation, one-stop purchasing is more efficient. A professional Floor heating manufacturer with full industrial and civilian product lines can provide supporting solutions. In addition to industrial heat tracing products, it also supports customized
electric heating mats for floors for factory staff dormitories and office spaces, realizing unified quality control and after-sales service for all heating systems.
Winter facility maintenance cannot rely on temporary remedies. Installing qualified heat trace cable is a long-term cost-saving investment. Unqualified low-cost products will cause pipeline failure and production shutdown losses far exceeding the procurement cost. When purchasing, you must focus on complete certification systems, factory production qualifications, and professional technical support.
A reliable supplier can provide 24-hour quotation response, professional engineering design guidance, and 2-25 years of free warranty service. Electric heating cable series products cover all industrial and civilian scenarios, solving various winter anti-freezing and heating pain points for global users. Whether it is industrial pipeline heat tracing, indoor floor heating, or outdoor snow melting and anti-icing, you can get targeted customized solutions here.
In conclusion, industrial heat trace cable is an essential guarantee for the stable operation of industrial pipelines in winter. Choosing certified, high-quality products and formal manufacturers can effectively avoid safety risks and economic losses, and create a safe and efficient production environment for enterprises.